Is It Necessary to Add a Fan to Blow Onto the Prusa Mk3 Power Supply?
PrusaSlicer 2.3 is out! At least, away the time you're watching this video (or reading this article ;-), it should be out, and it comes with newfound features like flat top infill, ironing, paint-on support material, and self-activating multivariate infill patterns.
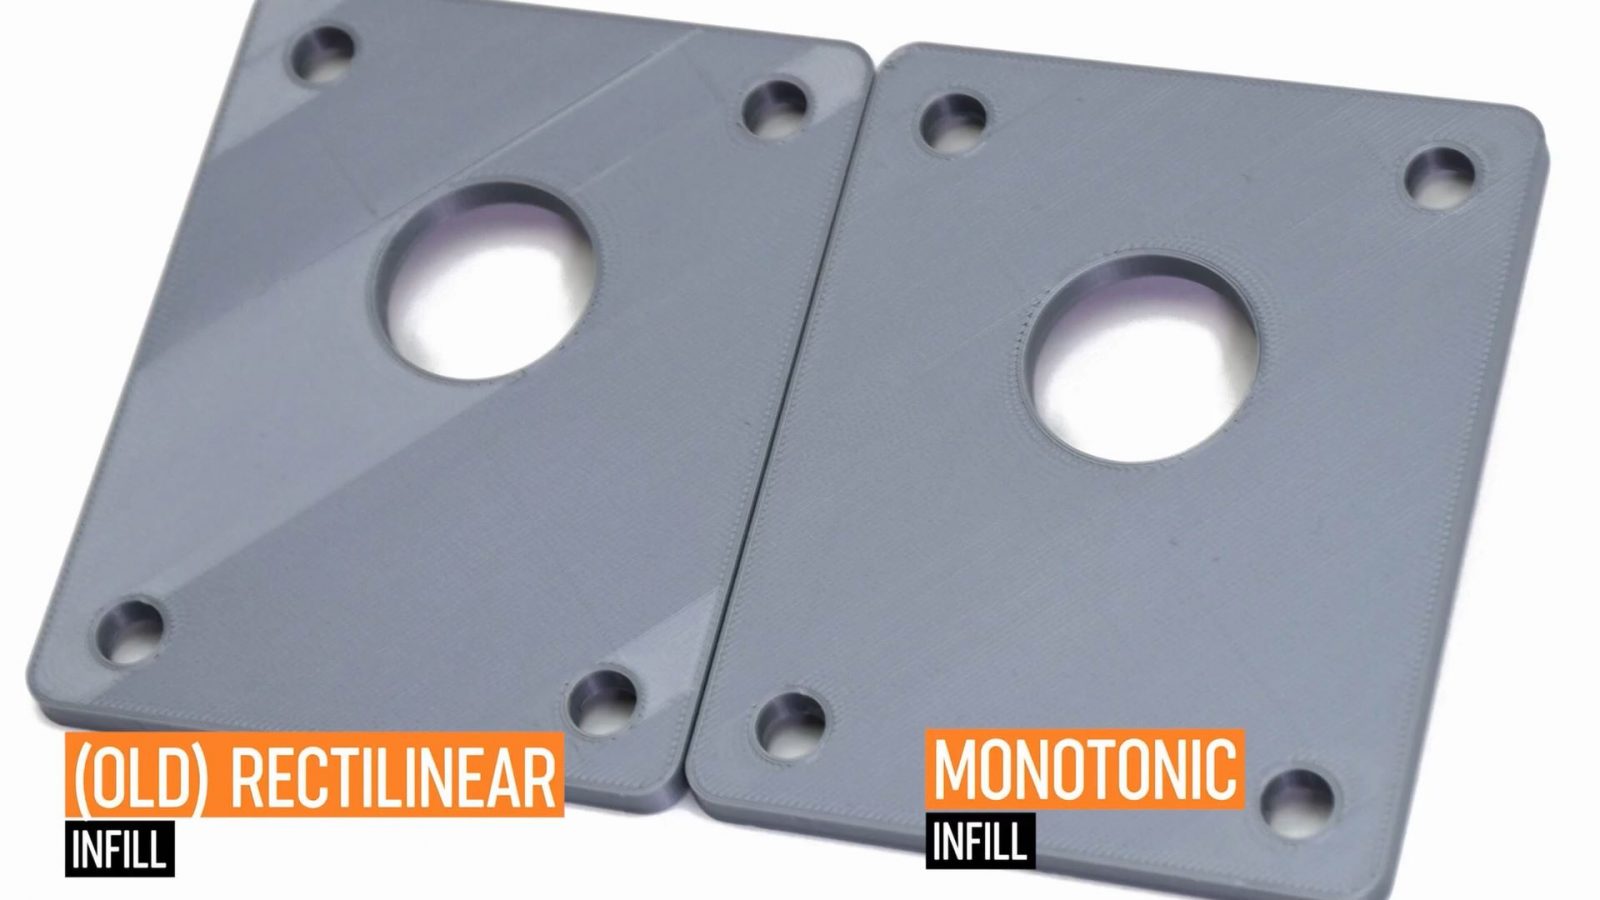
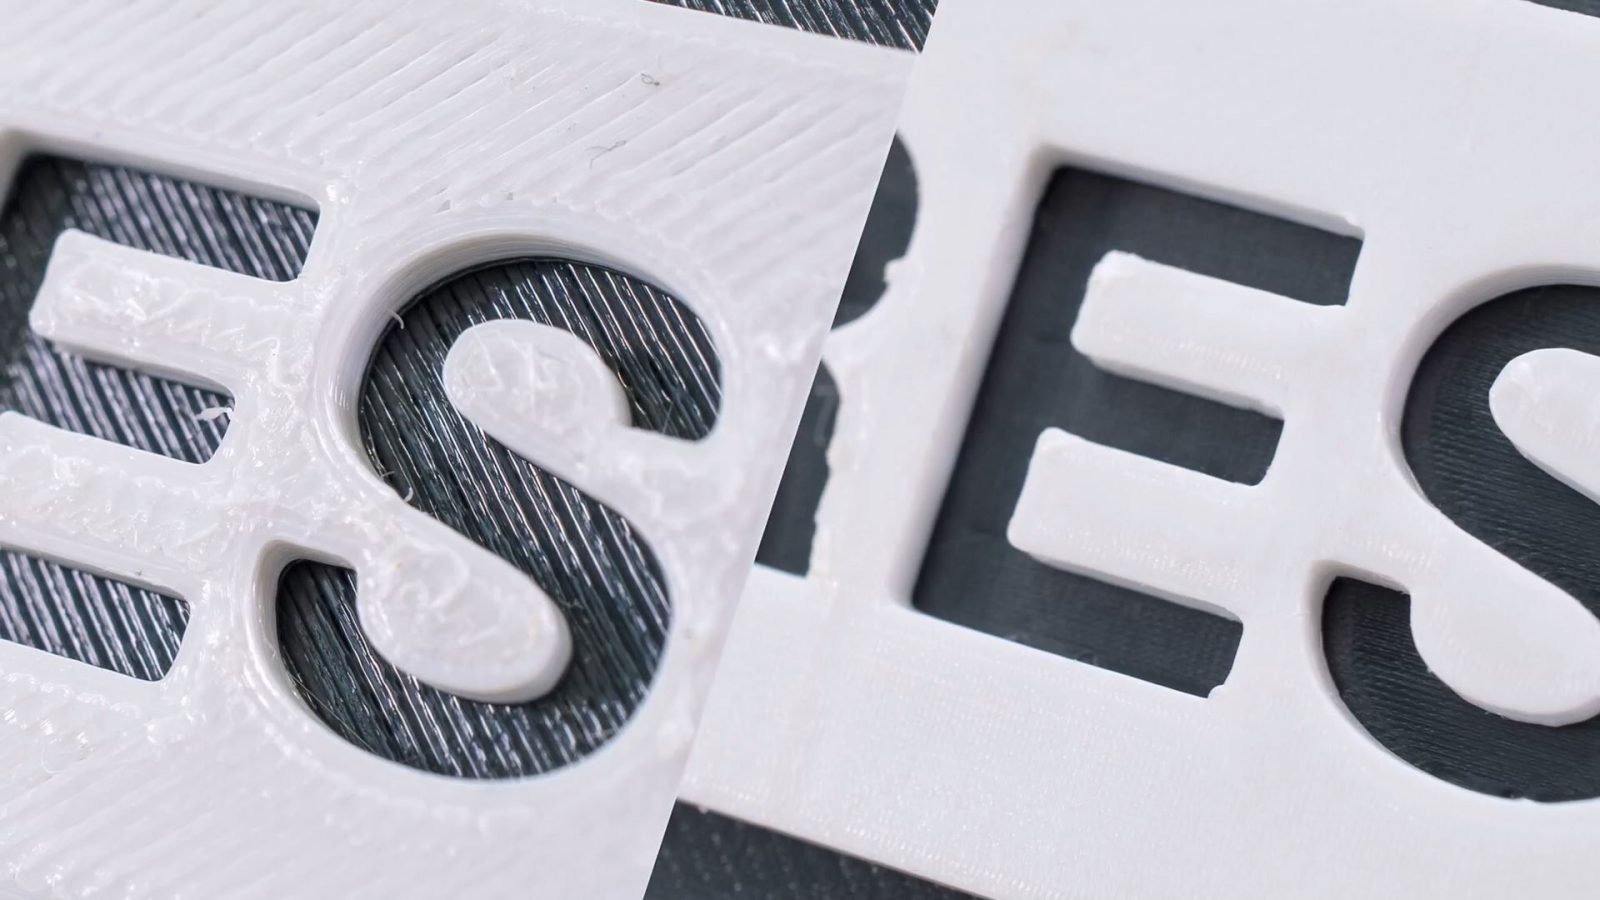
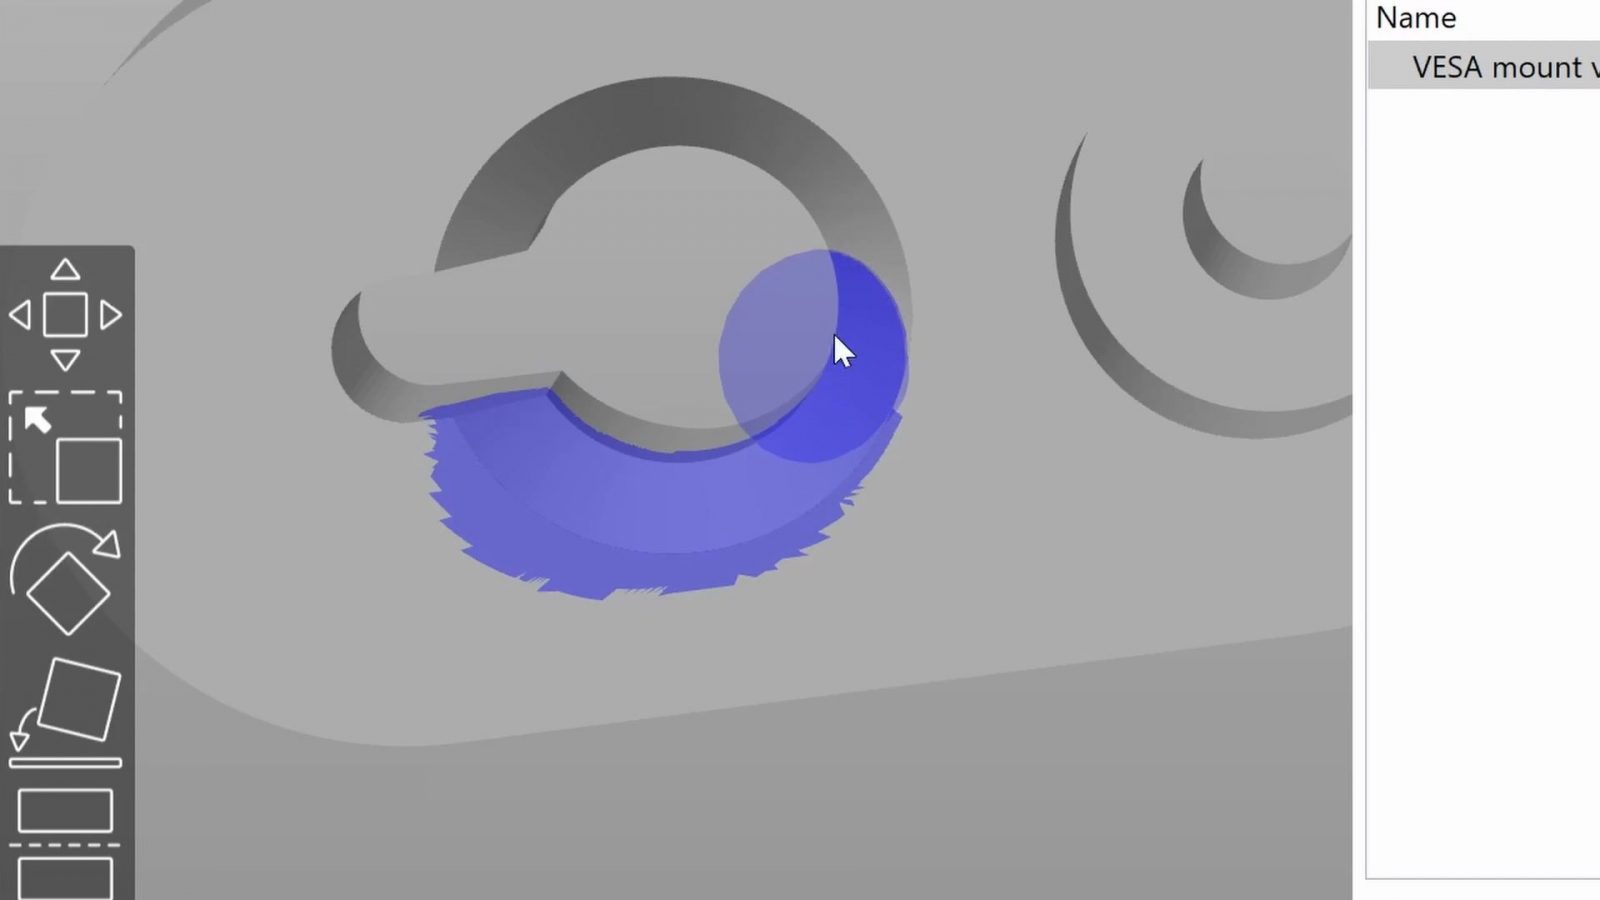
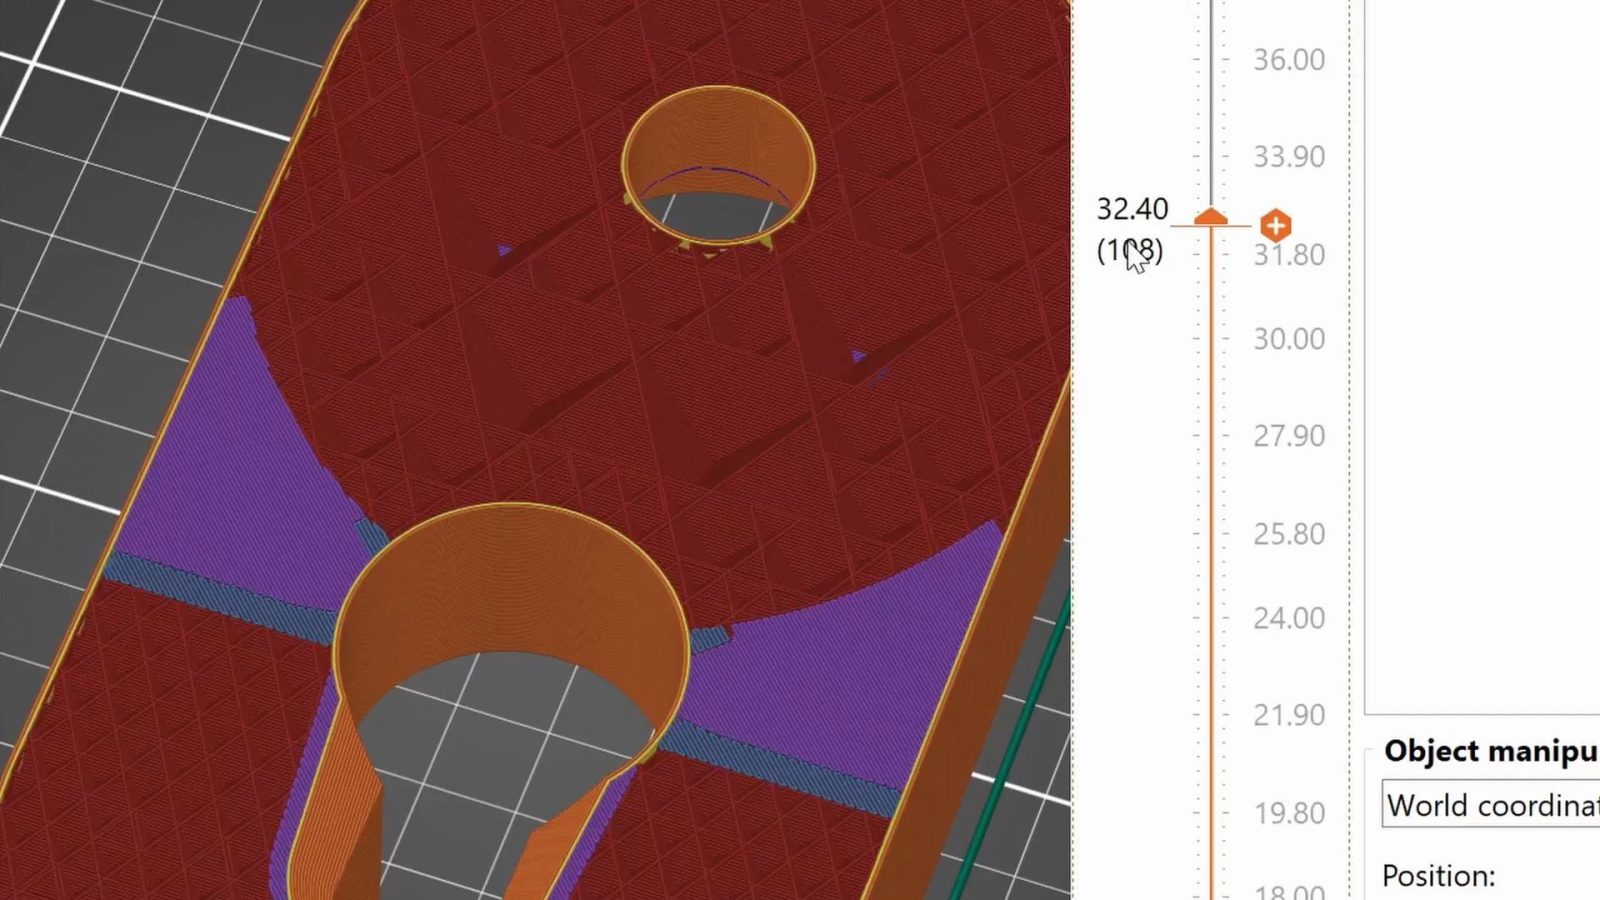
Here's the thing, though – PrusaSlicer and all the features it comes with are not selective to the Original Prusa 3D printers. In fact, Prusa really reached out and asked if they could sponsor this video where I show you how to set finished the new PrusaSlicer for basically any 3D printer. It's exempt and ASCII text file software, so this is basically a unpaid upgrade for the printer you already have.
Download and Set Up
Let's get right into it!
Step 1: Download and set u PrusaSlicer from prusa3d.com, you can get the stable versions right from the site, or, if you want the absolutely newest, unstable version, you grab that straight from the linked GitHub page.
Step 2: Run the configuration whizz. PrusaSlicer 2.3 is desegregation a lot more ready-made community profiles, and chances are you'atomic number 75 going to find a prepared-to-go visibility for maybe the right printer you have OR one that is similar plenty. For example, the Ender-3 profile is going to constitute a great starting point for the Ender-3 Pro, as well, Eastern Samoa well as the Ender-3 v2 and basically any other printer that is built like an Ender-3, which is… almost all of them, actually.
Run into finish, and that's IT – PrusaSlicer is immediately ready to employment for your printing machine. Thanks for observance, joyous holidays, and I'll… No, just kidding.
Custom Printer Options
I mean, this is a immaculate choice if your printing machine is already in at that place, just countenance's go through the "custom printer" option, and the changes I usually make, just to earn my life a bit easier. Too, we'rhenium going to steal both profiles from the Original Prusa machines.
So, in the constellation wizard, which you bathroom get under one's skin to through with the "Configuration" menu, the first affair to Doctor of Osteopathy is to in reality enable a profile for an New Prusa printer, for instance for the MK3S with a 0.4mm nozzle. We're going to need that by and by.
Then, of course, the future step is in the "Custom Printer" menu. First, choose a printing machine name, and then for the firmware, you're likely expiration to want to choose "Marlin", but some printers, especially when they'ray running weird, proprietary microcode, power deman RepRap/Sprinter selected hither in case they enactment up with the "Marlin" setting.
Next, for bed shape and size, just plop in the operational print area of your machine. Then, in "Filament and Nozzle Diameters", the default of 0.4mm for the snoot and 1.75mm for filament are correct for 99.9% of printers out there, and past, for temperatures, I like to go with a base 210°C at 60°C for PLA. Now, this wish create a new, very base filament profile, but since I'm leaving to show you how to snatch up profiles off of the MK3S, what you set up here doesn't matter much.
For now, hit "Finish" and you'll have new profiles for print settings, filament, and the printer. And you can completely use those or realise tweaks off of them, for example, I would recommend reduction the layer height from the 0.3mm that comes set up every bit default option, as well equally tuning downward speeds a trifle, as they'Re about 50% quicker than what is usually considered "safe" speeds to get good prints on most machines. But those adjustments won't get used when you use a diametrical print or strand visibility – however, the "Pressman" profile is one that we'Ra departure to prevent, so get's get this one dialed in. First things first, switch to the "Adept" view mode, which is going to show you all the settings useable. Once we're done setting everything up, you can always switch back to "Basic" or "In advance" mode to hide the settings you're not going to be using in any event. You don't have to, and actually, shouldn't tidy sum with a mint of these settings, but here are the ones that are important. In the "General" lozenge, set the maximum print height to the height your printer behind safely arrive at.
Then, in "Custom G-code", we're exit to set the start and end gcode, that is the commands the pressman always runs before and after the actual print. For the Start G-encipher, first of completely, if you take up a go to bed probe on your printer, you can run an auto-leveling pass by adding a bloodline with "G29" right after G28, which is just orientating. Past, if you want the beak priming delineate that the printer does at the front border of the bed ahead it starts the true photographic print, you're going to need to induce sure everything is preheated before it tries to perform that and that the printer then runs the actual priming line. And that looks the like this.
I'm also putting the full get going and end gcode in the video description so that you can just copy and paste it.
Now, for the end gcode, there are two things to add, first, for some reasonableness, past default IT's lost the command to unfriendly mastered the bed, that is M140 S0, and then, if you neediness the printing machine to move the black and white bed towards you when the black and white finishes, that's G1 Y200 F9001 – if you have a moving have it away on your printer, that is, otherwise, this is going to be active your toolhead back, which is fine, too, I guess.
Incoming, "Machine limits", my testimonial here is to change these to "Use for time estimate", because otherwise, several limits already hard in your printing machine may get overwritten, which stool cause issues with reliableness.
Lastly, in "Extruder 1", you'll find the "entertaining" settings, specifically for retraction. The default length is 2mm, merely for a direct-driveway extruder, I'd urge 1mm or less, for a Bowden, you plausibly wish around 4mm.
Enabling "Lift Z" with a lift height of 0.5mm is also a good idea unless your pressman's Z-axis is super surplus slow, just generally, this cuts down happening stringing a bit, keeps the nozzle from knocking over the print, and doesn't really impact print meter.
IT's considerate of the same with "Wipe away while retracting", right halt the box, it makes your prints a tiny bite nicer, and doesn't harm anything.
So, about the other deuce components of the PrusaSlicer config – the tabs called "Photographic print Settings" and "Filament Settings". Like I said, the settings in there moral now are usable, but PrusaSlicer comes with better profiles that, by default, are marked as only when being compatible with the Prusa 3D printers. But we can in reality tell PrusaSlicer something suchlike "you know, that matter about these profiles existence made for specific printers, they're not made for specific printers".
Keep in mind, though, that spell filament profiles work beautiful more than universally, the print settings profiles could need a number of fitting depending on your exact printer apparatus. Generally, though, they should atomic number 4 a bit many refined than the default profile that generates with a tailored printer setup.
So, to grab a profile from the MK3S, Army of the Pure's start with the print settings: Make sure to have the MK3S chosen as your topical printer, as fortunate as the visibility you want to copy. And so go into the print settings tab and all the way down at "Dependencies", sink in "come off from scheme planned", then yes, and pick a new name, something equivalent "0.15mm Quality Linguistic universal". Then, make sure the new profile is selected, which it will atomic number 4 by nonpayment, and check "all" for well-matched printers, and delete the line for compatibility conditions. Directly, if you prefer your custom-made pressman again, you'll see that you can now use the derived profile for that machine as well.
IT's look-alike for filament settings, again, make fated the MK3S is selected, then go to the filament profile you want to re-create, click detach, choose a new name, and then for the new profile, make in for both checkboxes are clicked to "all" and the text boxes are empty for the compatibility conditions.
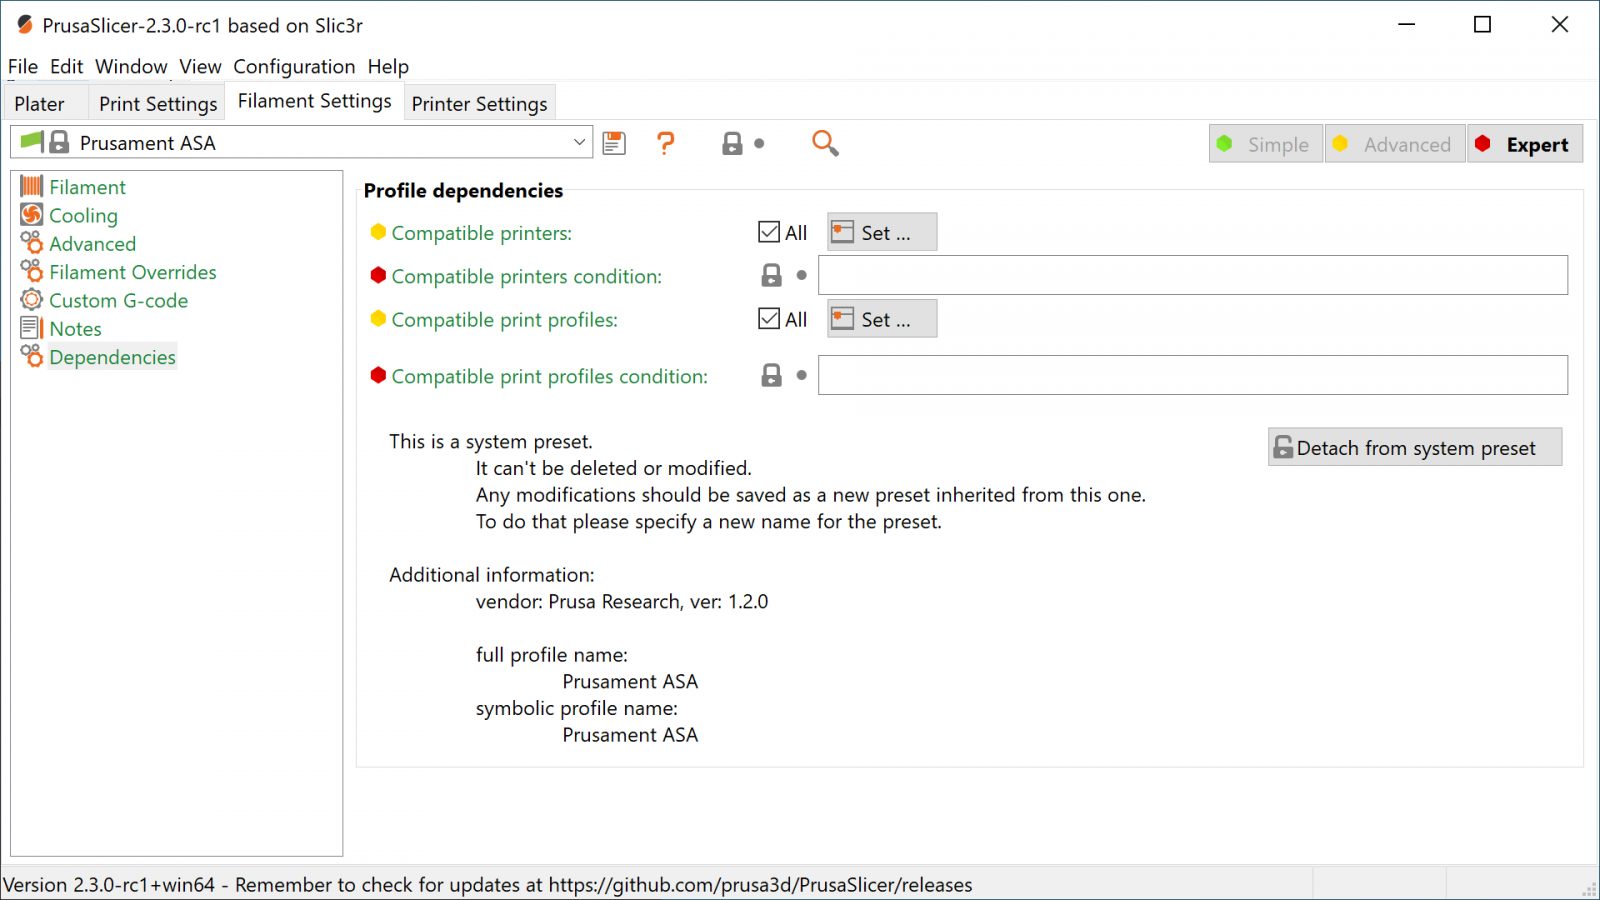
You should also check that in the "Bespoken G-code" settings, some boxes are empty – these settings are specific to the MK3S in this case. And also, for the "Filament Overrides" settings, these temporarily change some of the options in "mark settings" when you take this particularised fibril profile hand-picked. IT's a feature that can be very serviceable, but the settings in there right today are coiffe up for a direct-force printer, and then if you're using a Bowden printer or a printer where you think these overrides won't work, you should probably disable these.
And there you conk – you've got PrusaSlicer rear for your own printer with, what I think, is a really peachy, universal set of print settings. Now, over again, these might still need roughly tuning for your specific printer. The indefinite thing I like to do is to fill out upwards the first stratum to come through to a lesser extent alive to bed leveling errors, you fanny make this in "Print Settings" by profit-maximising the first layer height to about ¾ of your schnozzle size, so roughly 0.3mm, and likewise devising the extrusion track wider in the "Advanced" settings below "extrusion breadth", "first layer". I found that 1mm whole kit large here.
So what do you actually pose, right away that you're set up with PrusaSlicer? Here are some of the features that I chance super useful. First, what you already saw, the legal separation of print settings and filament settings. So you can have your profiles for fast printing process, printing process with supports, vase mode, etc, and then an mugwump set of profiles for printing with PLA, PETG, ASA, wood fill, etc, without having to create a single visibility for every mathematical combination of specific print settings and a filament.
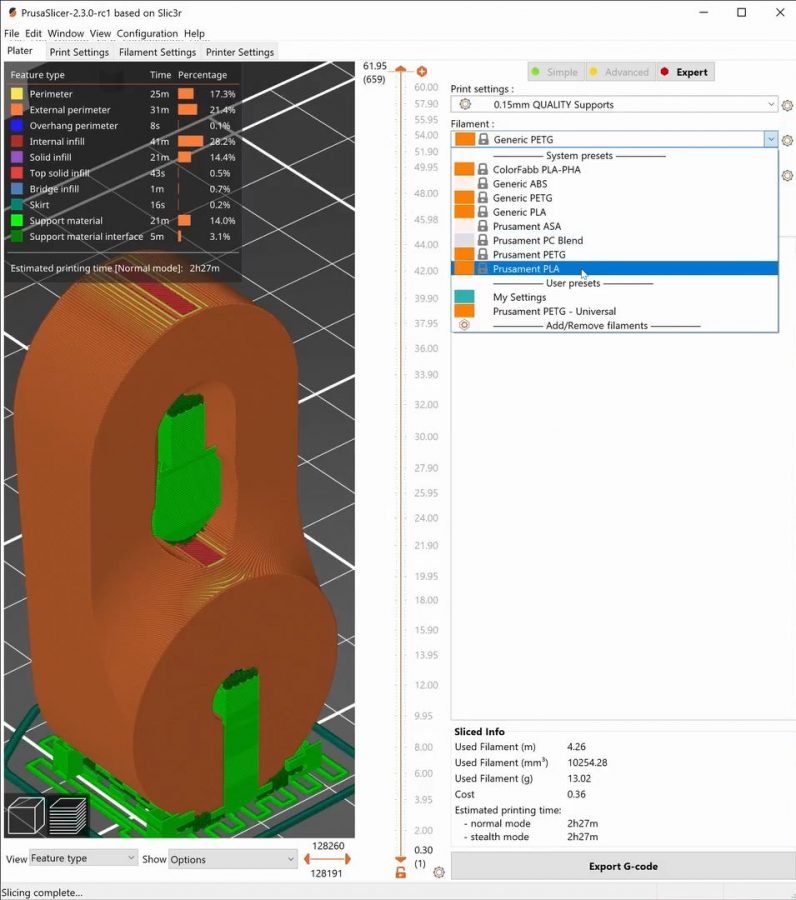
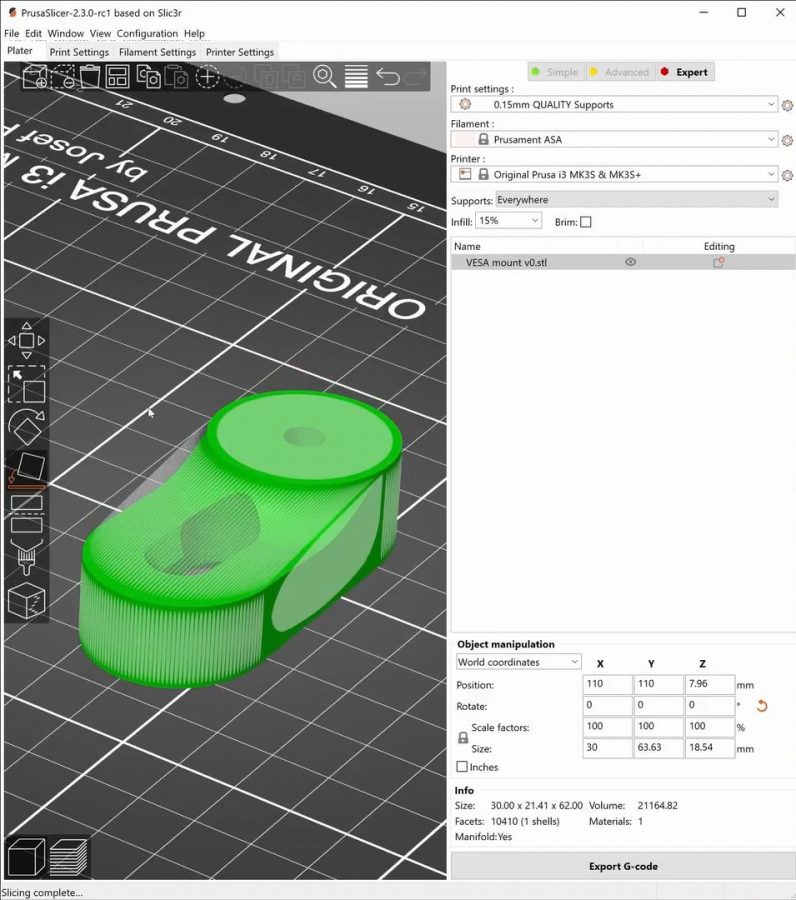
Then, in the plater, the absolute top timesaver is the lay-flat tool, you arse see it on the toolbar on the larboard here, and from in that location it's literally just a single click to rotate your part into the gross orientation for impression. That's and so much better than messing roughly with rotation handles. Which… you can stillness do, but why would you?
What I also use is "Ground processing", which you can enable in Contour – Preferences, which makes seeing what the antithetical settings do a mess faster. By the time you click indorse to the "Plater" tab, unremarkably, your part is already going to be sliced and ready with your refreshing settings.
And of course, there are the new options of using paint-on plump for material, ironing, reconciling cubic infill, just covering all those in contingent would follow its own entire video. If you want to learn to a greater extent just about them, Prusa already has videos aweigh, covering the new features.
At any rate, if you create a profile that works really healed for your specific printer, delight do share it with people that could make utilisation of IT as well, you can export and import profiles directly from the file menu. Or, if you're a manufacturer, there's an official guide of how you can make your own config bundle that can and so be enclosed with the official PrusaSlicer releases.
Thanks once again to PrusaResearch for sponsoring this video and thank you to all my Patrons for your continued support, without you, I really couldn't be making these videos. 2022 has been a vast learning experience for me, and honestly, things bathroom only get better in 2022. I would like-minded to thank you all so much for observance, like the video if you did, pledge to see more like it, keep fashioning, and I'll see you in the next twelvemonth. Golden holidays! Rest safe everyone.
Download PrusaSlicer
Manufacturer Frame-up guide
Start gcode:
(the [ ] sections will get full in away PrusaSlicer automatically in the exported gcode)
M104 S[first_layer_temperature] ; set extruder temp M140 S[first_layer_bed_temperature] ; set bed temporary M190 S[first_layer_bed_temperature] ; wait for bed temp M109 S[first_layer_temperature] ; await for extruder temporary G28 ; home all axes G29 ; autolevel G1 Z5 F5000 ; lift nozzle G1 Y0 F9001 ; attend nominal head edge of the bed G92 E0.0 ; reset extruder position G1 X60.0 E9.0 F1000.0 ; intro line G1 X100.0 E12.5 F1000.0 ; intro line G92 E0.0 ; reset extruder position End gcode:
M104 S0 ; plow unsatisfactory temperature M140 S0 ; turn off heatbed M107 ; turn remove fan G1 X0 Y200 F9001 ; nursing home X axis, immediate print M84 ; disenable motors 💙 Enjoying the videos? Support my make along Patreon!
Product links are affiliate links – I may earn a committal on limiting purchases (at atomic number 102 superfluous cost to you)
All my video gear mechanism
You seat support me without spending a single penny!
Is It Necessary to Add a Fan to Blow Onto the Prusa Mk3 Power Supply?
Source: https://toms3d.org/2020/12/28/prusaslicer-2-3/

إرسال تعليق for "Is It Necessary to Add a Fan to Blow Onto the Prusa Mk3 Power Supply?"